Five s lean manufacturing is hardest to sustain in plants that run two or three shifts. An area can be at standard when the day shift leaves and in disorder by the time it returns. Each shift blames the last, tools go missing between teams and the night shift often gets the least attention. This guide sets out five essential handover rules that keep five s lean manufacturing consistent across every shift.
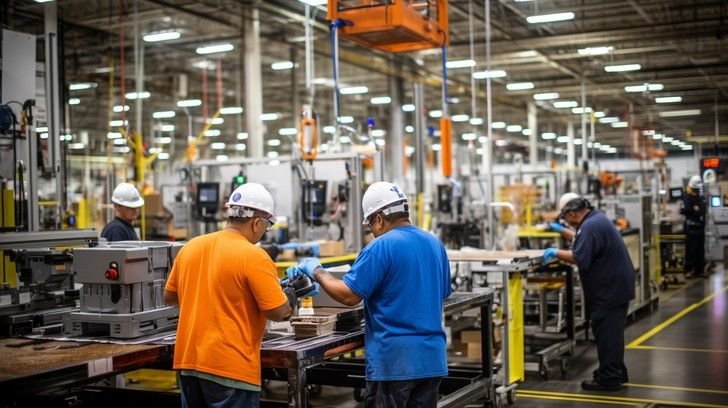
Many Indian plants run multiple shifts to make full use of equipment, from auto components and engineering to textiles, plastics and process industries. In these plants, the moment when one shift hands over to the next is where 5S standards are most often lost.
Why does five s lean manufacturing slip between shifts?
Five s lean manufacturing slips between shifts because responsibility becomes shared and therefore unclear. When an area is used by three different teams, each can assume another will put things back, clean up or report a problem. Small lapses build up over several handovers until the area no longer looks like the standard.
Other factors add to the problem. Shifts may have different supervisors with different expectations. Night shifts often have fewer support staff and less management attention. Handovers are rushed, focused on production numbers rather than the condition of the area.
Shift work is a fact of life in many plants. The aim is not to avoid it, but to design handovers so the standard passes cleanly from one team to the next.
| Common multi-shift problem | What it looks like | Rule that addresses it |
|---|---|---|
| Different standards by shift | Each supervisor accepts different conditions | Rule 1: one standard for every shift |
| Leftover mess at handover | Next shift starts by clearing up | Rule 2: reset before handover |
| Issues lost between shifts | Problems found at night forgotten by morning | Rule 3: a short structured handover |
| Blame between shifts | No one owns the area | Rule 4: named owners on every shift |
| Night shift neglected | Audits and visits only in day shift | Rule 5: equal attention for all shifts |
Rule 1: Why must every shift work to one standard?
The first rule is that every shift follows exactly the same 5S standard. Locations, labels, floor markings, cleaning tasks and storage limits should not change depending on who is in charge.
The easiest way to achieve this is a visual standard for each area, usually photos showing how each zone should look, displayed where everyone can see them. Supervisors from all shifts should agree the standard together and change it only together.
When standards differ, each handover becomes a negotiation. When they are the same, any difference from the photo is clearly a problem to fix, not a matter of opinion.
Rule 2: Why should every shift reset before handing over?
The second rule is that each shift returns the area to standard before handing over. Tools go back to their places, waste is removed, material is moved to its defined locations and machines are wiped down. The next shift should start from the standard, not from the previous team’s leftovers.
Build a fixed few minutes for this reset into every shift plan. If the reset is treated as optional when production is busy, it disappears exactly when it matters most.
The outgoing supervisor should check the reset before leaving. A simple walk with the incoming supervisor, comparing the area with the standard photos, makes the condition of the area part of the handover.
Rule 3: What should a shift handover include for 5S?
The third rule is to include 5S in a short, structured shift handover. Most handovers already cover output, quality issues and machine problems. Adding the condition of the area and any open 5S issues takes very little extra time.
A simple handover board in each area helps. It shows open issues, such as a broken shadow board, a missing label or a recurring spill, with the person responsible and the target date. Each shift updates the board, so problems found at night are still visible in the morning.
This links naturally with a structured daily work management routine, where each shift’s issues feed into the next shift’s briefing and the daily review.
Rule 4: How should ownership work across shifts?
The fourth rule is to name an owner for each zone on every shift. When an area is shared, a named person on each shift is responsible for its condition during that shift and at handover. A single overall area owner, often the day shift supervisor or area in-charge, holds the standard across all shifts.
Named ownership reduces blame. If a zone is not at standard at handover, it is clear which shift needs to act. Over time, this encourages each team to leave the area as they would like to find it.
Ownership also works best when shifts meet occasionally. A short monthly meeting of supervisors from all shifts to review the area and agree improvements builds shared responsibility rather than competition.
Rule 5: How do you give every shift equal attention?
The fifth rule is that audits, visits and recognition cover every shift, not just the day shift. In many plants, managers see the area only during the day, so night shift problems stay hidden and night shift efforts go unnoticed.
Rotate audits across shifts, including occasional night checks by senior staff. Share results by shift so teams can see how they compare, while focusing on learning rather than blame. Recognise good performance on every shift.
Night shifts often face extra challenges, such as fewer support staff or limited access to stores and maintenance. Asking night teams what gets in the way of keeping the standard often reveals practical problems that can be fixed easily.
But there is a more fundamental question worth asking: in your plant, does the 5S standard belong to the area, or to whichever shift happens to be working there?
When it belongs to the area, every shift protects it. When it belongs to the shift, it changes every eight hours.
How do supervisors coordinate 5S across multi-shift plants?
Supervisors in multi-shift plants need a simple way to stay aligned. A shared standard, a common handover board and a regular meeting between shift supervisors go a long way.
It also helps if supervisors occasionally overlap or swap shifts. Seeing the area through another shift’s eyes builds understanding of the problems each team faces and reduces the tendency to blame.
Plant leaders can support this by reviewing 5S results across all shifts together, rather than shift by shift, and by treating the area as one unit with one standard.
What does good shift handover look like in practice?
A good handover takes only a few minutes. The outgoing and incoming supervisors walk the area together, compare it with the standard photos, review the handover board and agree any actions. The incoming shift then starts work in an area that is ready.
Over time, the handover becomes routine and quick. Most days there is little to discuss because each shift has kept the standard. When problems do appear, they are caught at the handover rather than discovered hours later.
For more on building the basic 5S standard that handovers protect, the 5S in lean manufacturing guide and the 5S visual workplace overview are useful starting points.
What tools help five s lean manufacturing across shifts?
A few simple tools make the handover rules easier to follow. Standard photos of each zone, displayed at the entrance to the area, show every shift exactly what good looks like. Shadow boards with outlines for each tool make missing items obvious at a glance.
A handover board, either a whiteboard or a printed sheet, keeps open issues visible from one shift to the next. Colour-coded floor markings show where material, waste and finished goods belong, so nobody needs to remember or guess.
Some plants add a short checklist for the end-of-shift reset, listing the few points each team must confirm before leaving. Kept brief, it helps new or temporary workers learn the standard quickly.
None of these tools needs much investment. What matters is that every shift uses the same ones in the same way, so the area looks and works the same whoever is on duty.
Frequently asked questions
How long should the end-of-shift 5S reset take?
Usually only a few minutes if the standard is kept during the shift. If it takes much longer, the area is drifting during the shift and needs more attention earlier.
Who owns 5S in an area used by three shifts?
One overall area owner holds the standard, with a named person responsible on each shift for the area’s condition and the handover.
How do you stop blame between shifts?
Use one standard, a joint handover walk and a shared issues board. When facts are visible to everyone, discussions focus on fixing problems rather than blaming the last shift.
Should night shifts be audited?
Yes. Rotating audits across all shifts, including occasional night checks, shows that the standard applies equally and helps uncover problems specific to night work.
Conclusion: five s lean manufacturing that survives every handover
In multi-shift plants, five s lean manufacturing is won or lost at the handover. Use one standard for every shift, reset before handing over, include 5S in a short structured handover, name owners on every shift and give all shifts equal attention. Together, these five essential rules help the standard pass cleanly from one team to the next, day and night.